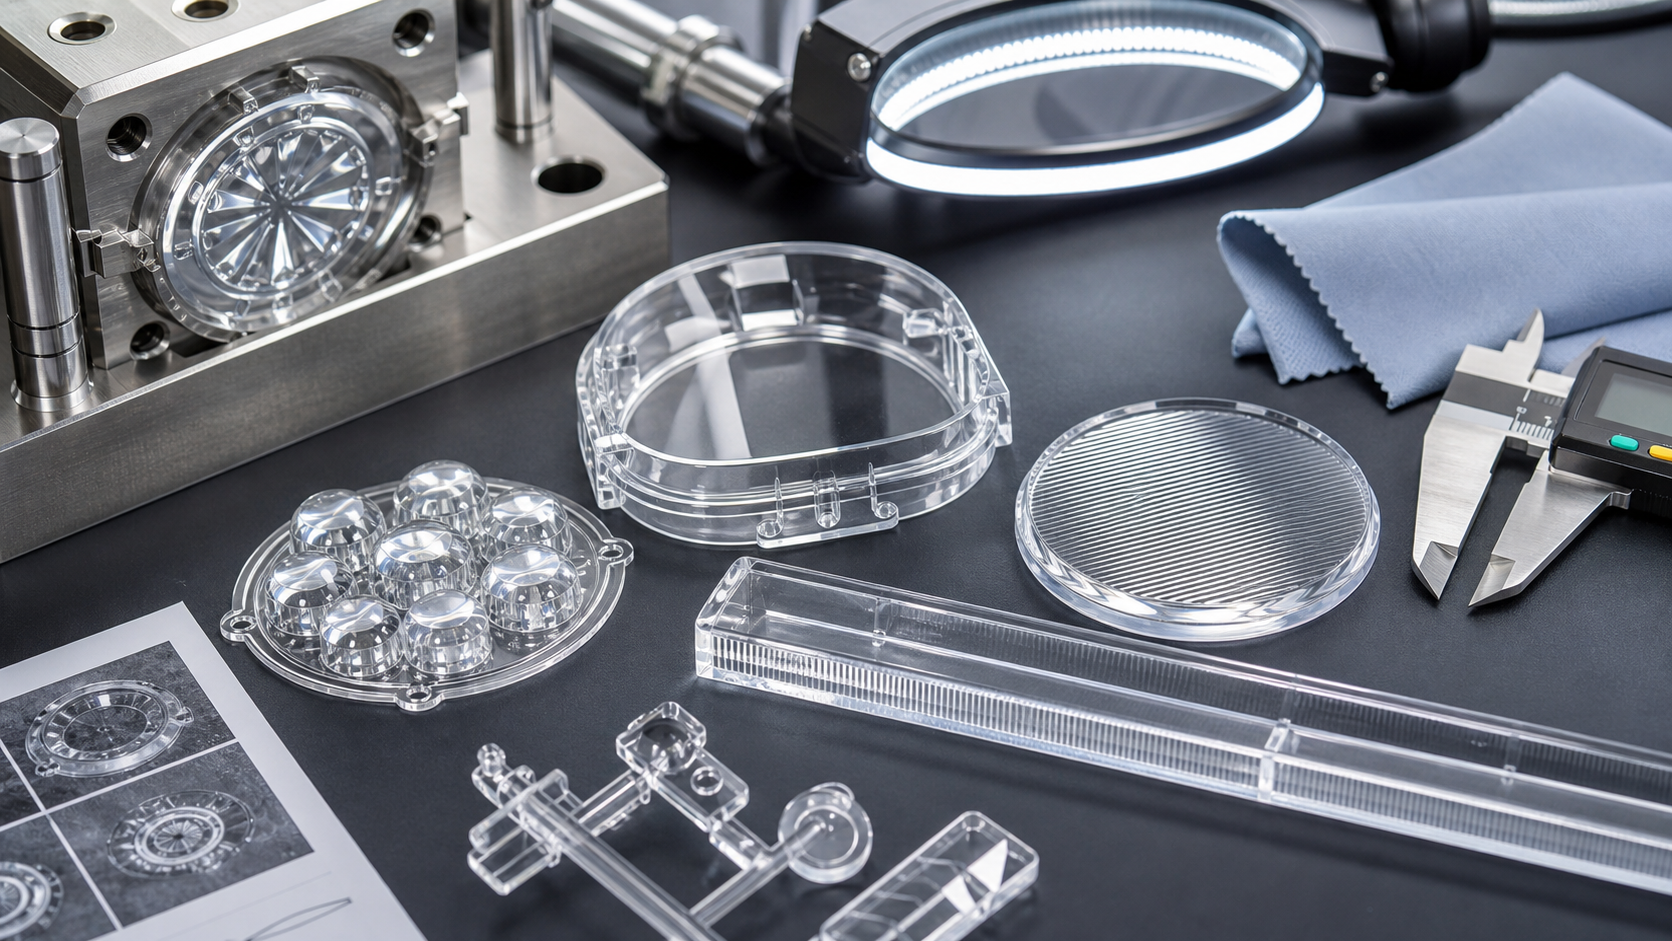
PMMA injection molding is used for acrylic clear parts such as lenses, light guides, covers, windows and display components. PMMA offers excellent optical clarity and surface hardness, but it needs careful drying, polishing, gate design and stress control to avoid bubbles, flow marks, sink, scratches and cracking.
A clear molded part is judged differently from a hidden bracket. Small defects that would be acceptable in black ABS can be rejected in PMMA because light transmission, distortion and surface appearance are part of the function.
Where PMMA Works Well
PMMA is chosen when clarity, gloss and scratch resistance matter more than extreme impact strength.
| Part type | Why PMMA is used | Design concern |
|---|---|---|
| Light guide | High clarity and good light transmission | Gate vestige and flow lines must be controlled. |
| Transparent cover | Glossy clear surface | Avoid scratches and internal stress. |
| Lens or window | Optical quality and hardness | Mold polish and part thickness matter. |
| Display component | Clear appearance and stable surface | Packaging and handling can cause scratches. |
| Decorative clear part | High gloss and colorability | Avoid sink and weld line visibility. |
PMMA Clear Part DFM and Sample Approval
For acrylic injection molding, define whether the component is a cosmetic cover, a viewing window or a light-transmitting part. Identify the exact molding grade, clear or tinted appearance and any permitted substitution. Compare grade data at the relevant thickness and test condition; a resin datasheet does not by itself approve the finished optical part.
- Place gates where vestige and flow marks are acceptable.
- Avoid abrupt wall transitions that create sink or optical distortion.
- Specify mold polish level for optical surfaces.
- Control drying and material handling to reduce bubbles and splay.
- Review packaging, handling and protective film for scratch prevention.
Mark visible and functional optical surfaces on the drawing. Agree inspection lighting, viewing distance, acceptable gate and ejector locations, and a reference sample or defect limit for scratches, bubbles and flow marks. Where light transmission, haze, distortion or assembled illumination is functional, specify the test and acceptance limit. An approved appearance sample should accompany the drawing revision used for production.
PMMA vs PC for Clear Molded Parts
PMMA usually wins on optical clarity and scratch resistance, while PC is often selected for impact strength and toughness.
| 素材 | 強さ | Limitation |
|---|---|---|
| PMMA / acrylic | Excellent clarity, gloss and surface hardness | Lower impact strength than PC. |
| PC | High impact resistance and toughness | More prone to scratching and stress issues. |
| Transparent ABS blend | Cost and toughness balance in some designs | Lower optical clarity. |
| CNC machined acrylic | Good for prototypes and low volume | Higher unit cost at scale. |
| 3D printed clear material | Fast concept validation | Usually lower optical quality. |
関連記事
For clear parts, decide early whether the project needs CNC prototypes, 3D printed samples, injection molded PMMA or injection molded PC.
よくある質問
Is PMMA good for injection molded clear parts?
Yes. PMMA is widely used for clear molded parts because it offers high optical clarity, gloss and surface hardness.
What defects are common in PMMA injection molding?
Common PMMA defects include bubbles, splay, flow marks, sink, scratches, internal stress, gate marks and optical distortion.
Is PMMA stronger than polycarbonate?
PMMA has better scratch resistance and clarity, but polycarbonate is much tougher and more impact resistant.
Does PMMA need drying before molding?
Yes. PMMA should be dried according to grade recommendations to reduce bubbles, splay and optical defects.
Request an Acrylic Injection Molding Review
Nylon Plastic supports material selection and custom plastic-part manufacturing. For a clear cover, window or light guide, send the CAD and drawing revision, prototype or production quantity, and target timing. For a material-only request, identify the current grade and required optical, impact or exposure performance.
Include the visible-surface map, approved appearance reference, critical fits, exact PMMA grade or permitted alternatives, and any optical test required for sample acceptance. State the destination, protective packaging and required inspection records.
The review can clarify grade, gate, finish and approval questions before quotation. Ask the quote to separate tooling and polishing, cavity count, sampling, molded-part supply, inspection and protective packaging. Confirm tool ownership and any excluded optical validation or secondary finish. A clear CNC or printed prototype may help check geometry; its appearance does not approve the molded production part.