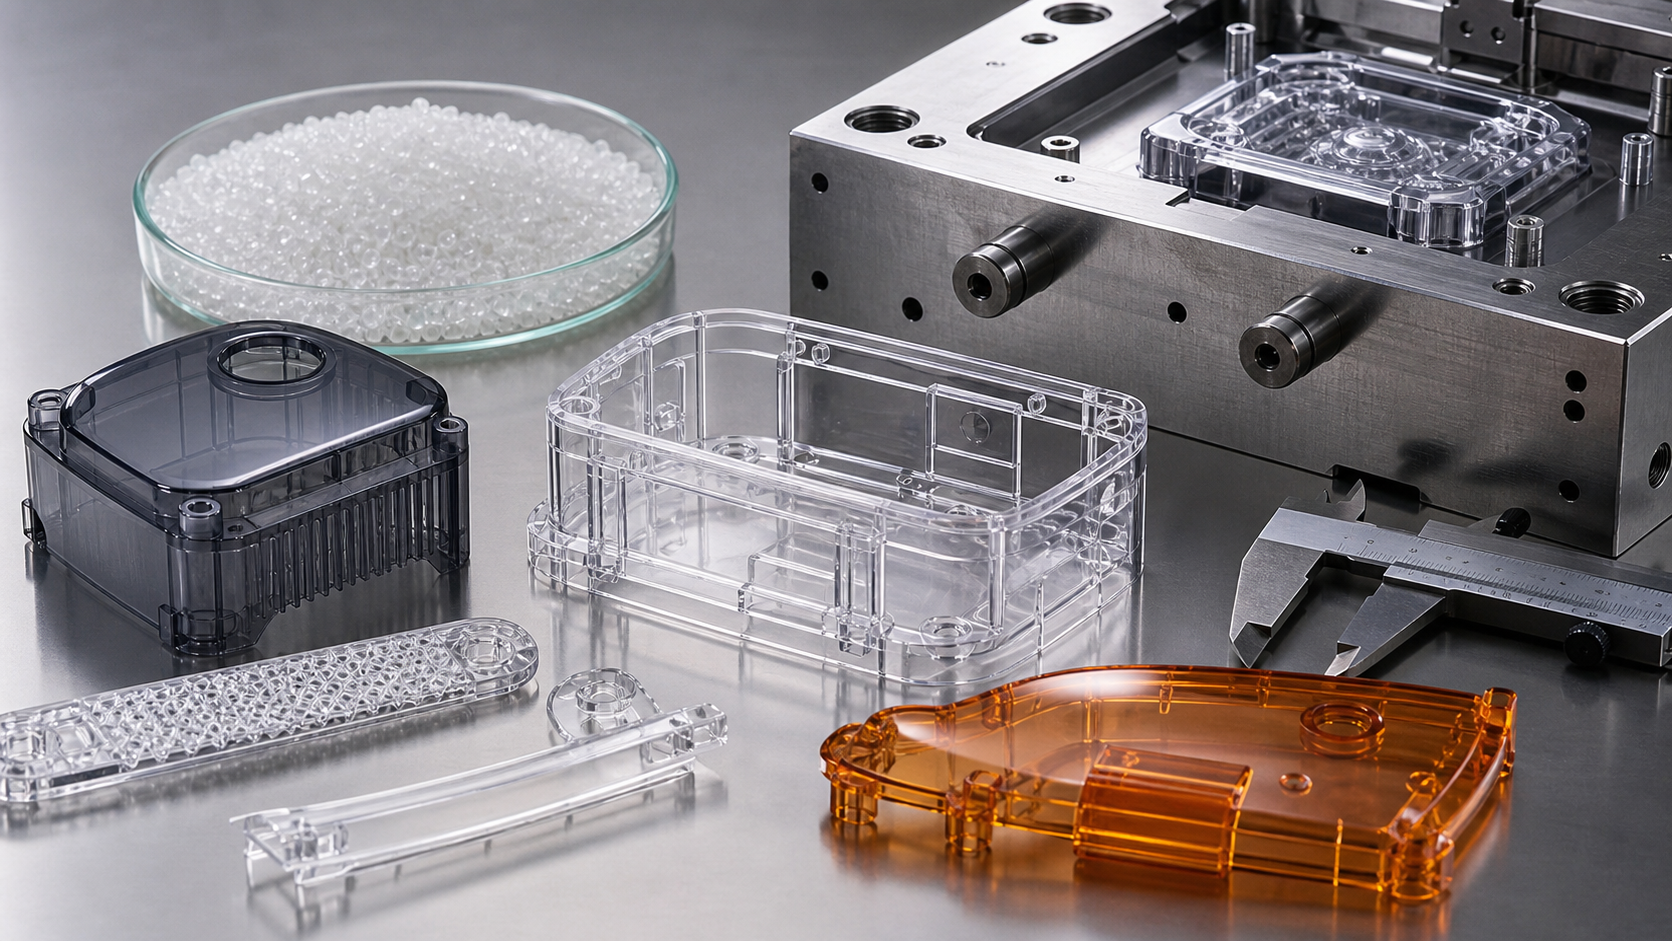
Polycarbonate injection molding is used when a custom plastic part needs high impact strength, heat resistance or transparency, but PC requires proper drying, mold temperature control and stress-aware design.
PC is tougher and more heat-resistant than many commodity plastics, but it is also more sensitive to moisture, residual stress and processing conditions. A good DFM review helps avoid splay, brittleness, optical defects and cracking around sharp corners.
PC Injection Molding Process Considerations
PC molding should be planned around drying, melt temperature, mold temperature, venting, packing and controlled cooling.
| ルート | 最適な用途 | 購入者への注意事項 |
|---|---|---|
| Transparent PC molding | Covers, lenses and light pipes | Needs optical and cosmetic requirements |
| Impact-resistant PC molding | Protective housings and guards | Review corner radius and stress concentration |
| PC-ABS molding | Tough housings with better processability | Consider when full PC is not required |
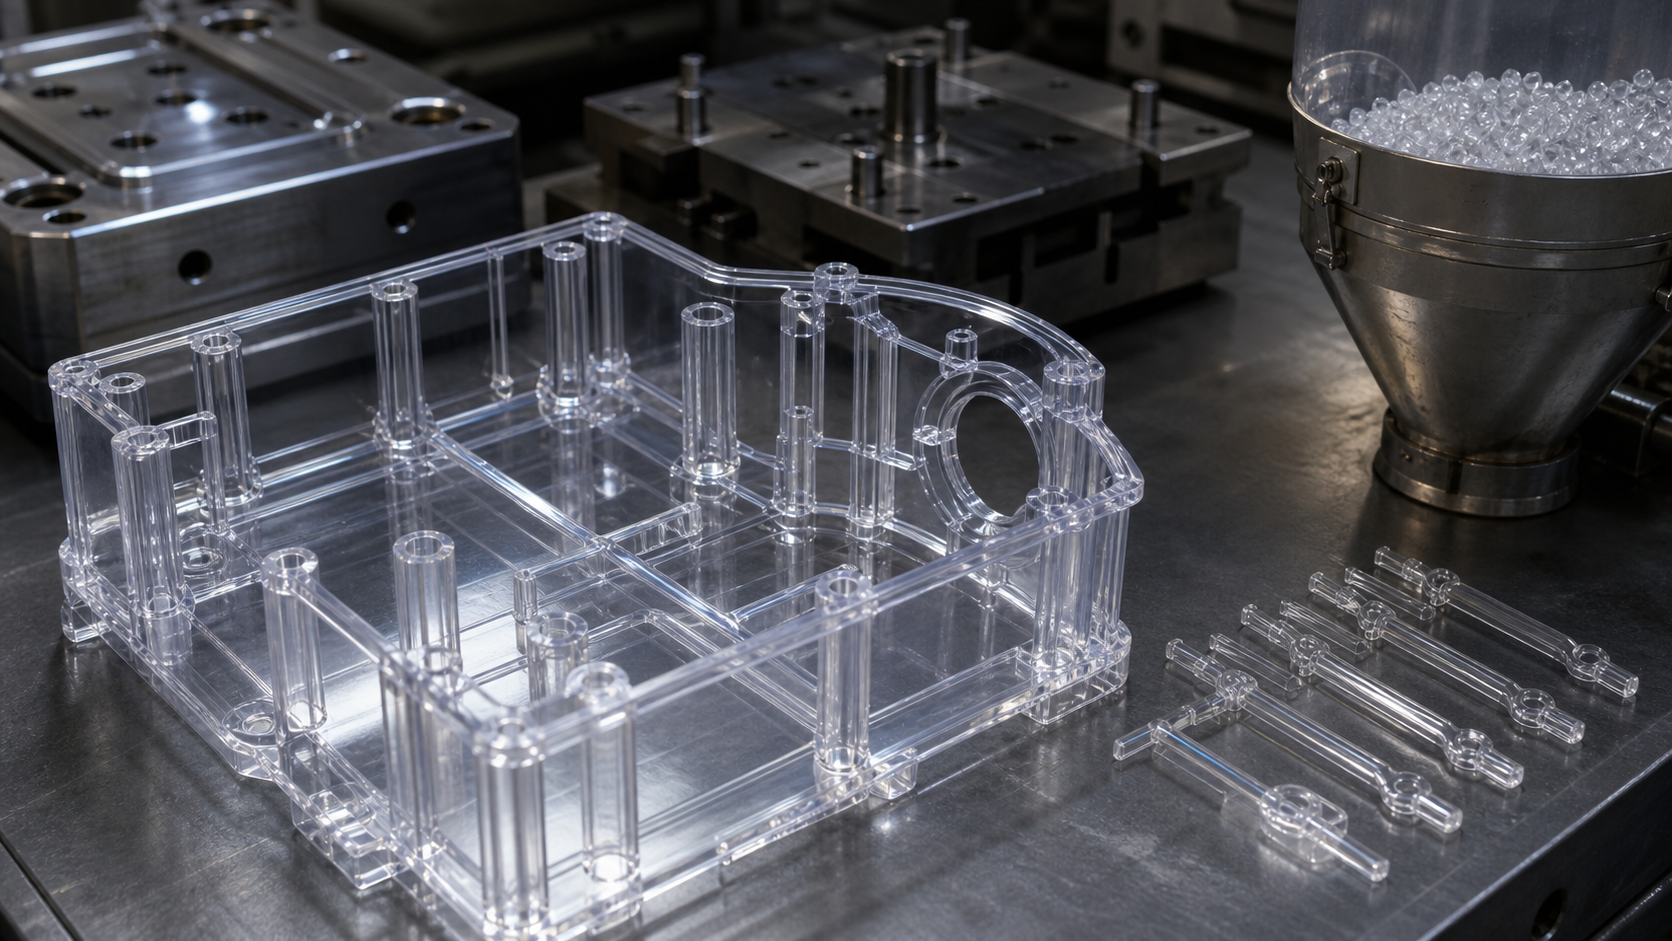
PC Grades and Related Materials
The best PC grade depends on transparency, impact, heat, flame resistance, UV exposure and cosmetic expectations.
| 素材 | こんな方に最適 | 選定に関する注記 |
|---|---|---|
| Clear PC | Transparent covers and lenses | Control drying, stress and scratches |
| UV-stabilized PC | Outdoor transparent parts | Review yellowing and exposure time |
| FR PC | Electrical and safety components | Confirm flame rating and wall thickness |
| PC-ABS | Tough housings | Often easier to mold than pure PC |
DFM Checks for Polycarbonate Parts
PC part design should reduce stress concentration and avoid features that trap flow marks or create cracking risk.
- Dry PC resin before molding to reduce splay and brittleness.
- Use generous radii around loaded features.
- Avoid sharp notches near screw bosses and snap fits.
- Define optical surfaces separately from structural surfaces.
- Confirm whether annealing or post-processing is needed.
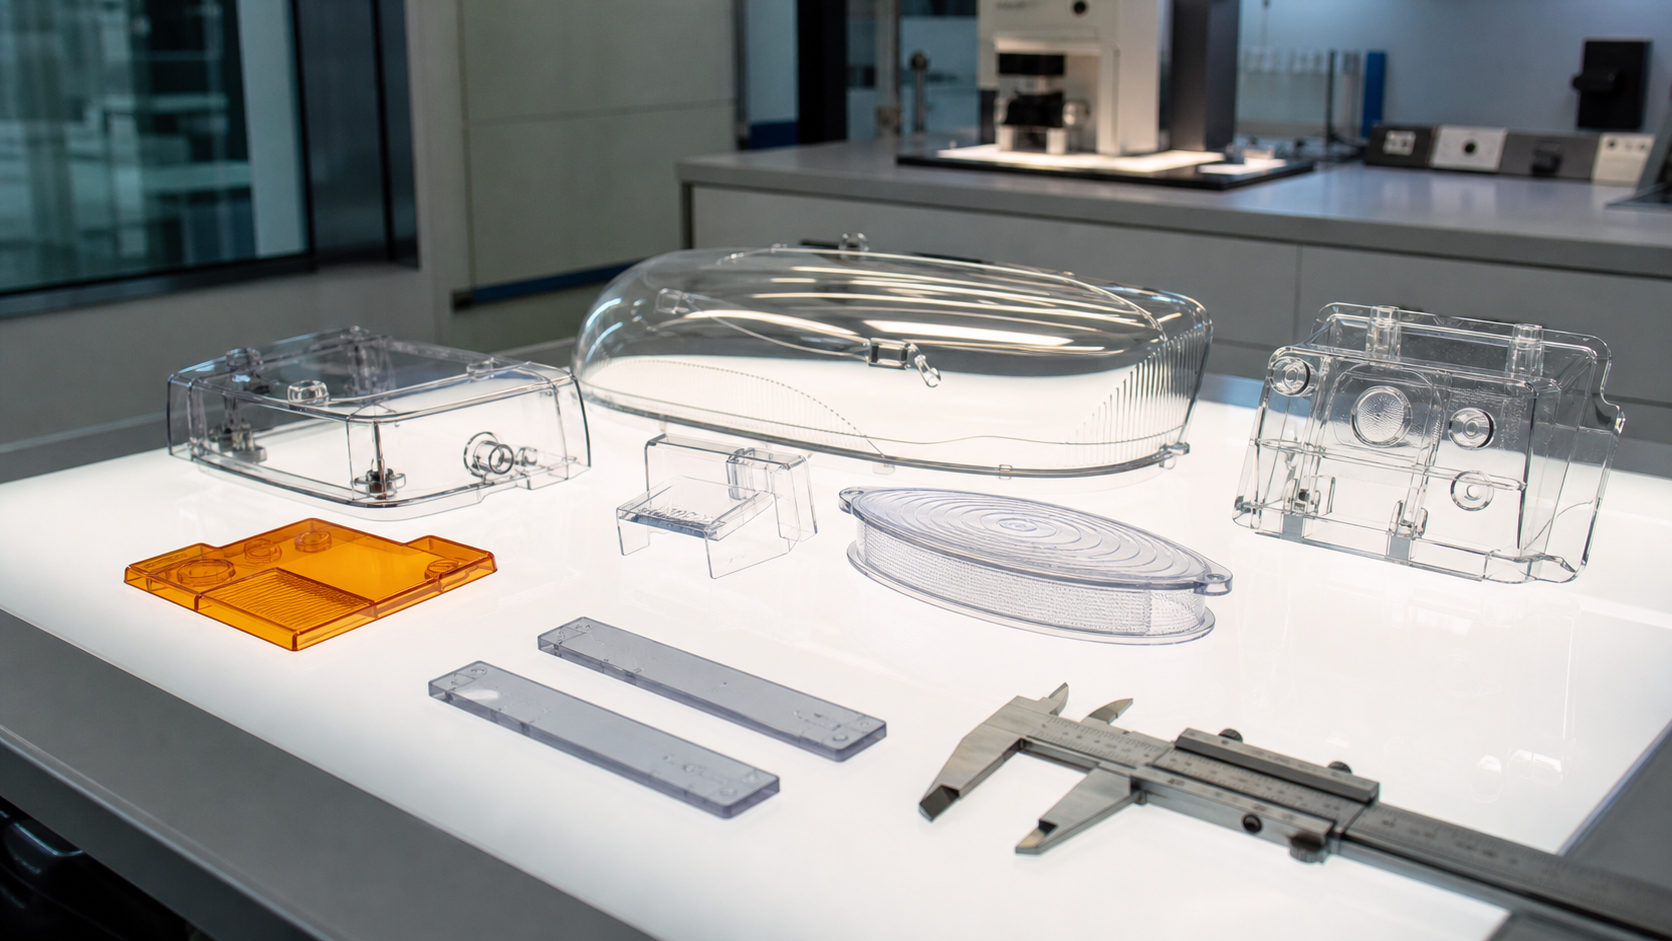
For a polycarbonate molding project, confirm resin drying, melt temperature, mold temperature, gate design, venting and residual stress controls before tooling release. For broader process planning, review our プラスチック射出成形サービス capabilities and include the application environment, annual volume and critical dimensions in the RFQ.
PC Injection Molding Processing Checks
| ファクター | その重要性 | Buyer / DFM note |
|---|---|---|
| 乾燥 | PC is moisture sensitive and can show bubbles, splay or reduced strength if not dried. | Confirm resin drying conditions before sampling. |
| 金型温度 | Higher mold temperature improves surface quality, flow and stress control. | Critical for clear, glossy or tight-tolerance parts. |
| Gate design | High shear can create blush, stress marks or visible flow defects. | Review gate size, gate location and weld line position. |
| Residual stress | Stress can cause cracking during assembly, coating or chemical exposure. | Avoid sharp corners, forced assembly and aggressive cleaners. |
Common PC Molding Defects and Fixes
| 欠陥 | Likely cause | Correction path |
|---|---|---|
| Splay or bubbles | Moisture, overheating or trapped gas. | Improve drying, lower residence time and check venting. |
| Gate blush | High shear at a small or sharp gate. | Increase gate area, polish transition and adjust fill speed. |
| Sink or voids | Thick walls, bosses or early gate freeze. | Core out thick areas and review packing path. |
| Cracking | Residual stress, sharp corners or chemical contact. | Improve radii, reduce stress and validate chemical exposure. |
DFM Checklist for Polycarbonate Parts
- Use consistent wall thickness to reduce sink and residual stress.
- Place gates away from optical or high-cosmetic surfaces when possible.
- Use generous radii around snap fits, screw bosses and loaded corners.
- Confirm draft, polish and texture expectations before mold cutting.
- Review chemical exposure, especially cleaners, oils, solvents and coatings.
- Compare PC, PC/ABS and PMMA if the part is transparent or cosmetic.
よくある質問
What is polycarbonate injection molding used for?
Polycarbonate injection molding is used for transparent covers, impact-resistant housings, guards, lenses and parts that need toughness or heat resistance.
Why does PC resin need drying before molding?
PC is moisture sensitive. Poor drying can cause splay, bubbles, brittleness, optical defects and reduced part performance.
What design issues matter for PC molded parts?
PC designs should avoid sharp notches, stress concentration, poor boss design and cosmetic surfaces that are not protected from flow marks or scratches.
When should PC-ABS be considered instead of PC?
PC-ABS can be considered when the part needs toughness and processability but does not require the full transparency or performance of pure polycarbonate.
関連記事
Request a PC Molded-Part Review
For transparent covers, housings, guards or lighting components, send the controlled drawing, exact PC grade or permitted alternative, and quantity by phase. Nylon Plastic can review material selection, tooling, drying, sampling and inspection before quotation.
What information helps quote clear polycarbonate injection molding parts?
Mark optical areas, permitted gate marks, polish or texture, viewing direction, assembly loads and cleaning chemicals on the drawing. Include the exact PC grade or the required transparency and performance. Ask the quote to distinguish molding from polishing, coating, assembly and cosmetic inspection, and agree an appearance reference before releasing the tool.
- Include CAD, revision, critical fits, color, initial and annual quantity, destination and target timing.
- State required optical tests and viewing conditions, permitted scratches or gate marks, assembly loads, cleaners and coatings.
- Match flame, UV or regulatory requirements to the exact grade and relevant part thickness; specify the documents and sample records needed.
Agree whether the quote includes mold polish, part finishing, coatings, assembly and optical or cosmetic testing. A general transparent-PC datasheet does not establish a finished lens or assembly acceptance limit.