This nylon injection molding services guide explains material selection, tooling review, tolerance planning, defect prevention, and RFQ details for custom molded PA6, PA66, and glass-filled nylon parts.
For the broader production workflow, tooling options and quality process, see our プラスチック射出成形サービス page.
What Are Nylon Injection Molding Services?
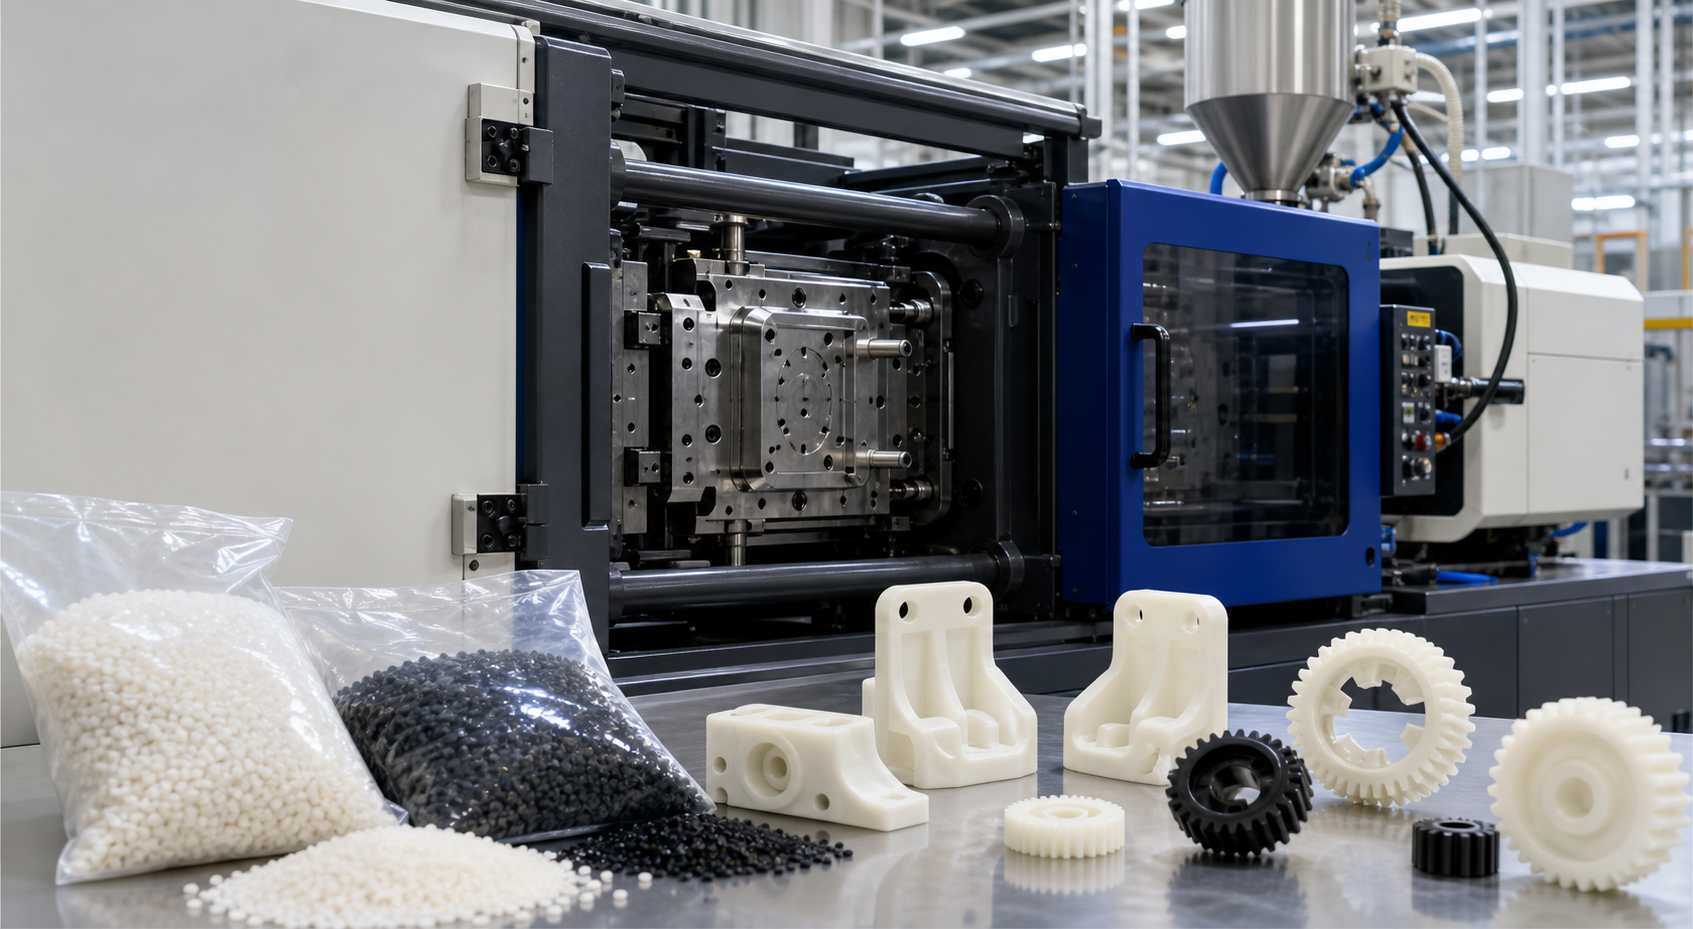
Nylon injection molding services turn PA6, PA66, glass-filled nylon and other engineering polyamides into custom production parts using precision molds. A qualified supplier should support material selection, DFM review, tooling strategy, drying control, molding trials, dimensional inspection and production delivery.
For buyers, the real question is not only whether nylon can be molded. The key question is whether the chosen nylon grade, mold design and process window will keep the part stable after moisture absorption, heat exposure, mechanical load and assembly.
At Nylon Plastic, nylon molding projects often start with a practical review of resin behavior, wall thickness, gate position, tolerance targets and expected production volume. That early review prevents many avoidable trial loops.
Nylon Injection Molding at a Glance
| 要件 | Common nylon choice | その重要性 |
|---|---|---|
| General tough molded parts | PA6 | 優れた靭性と加工性 |
| Higher heat resistance | PA66 | Better thermal performance than PA6 in many applications |
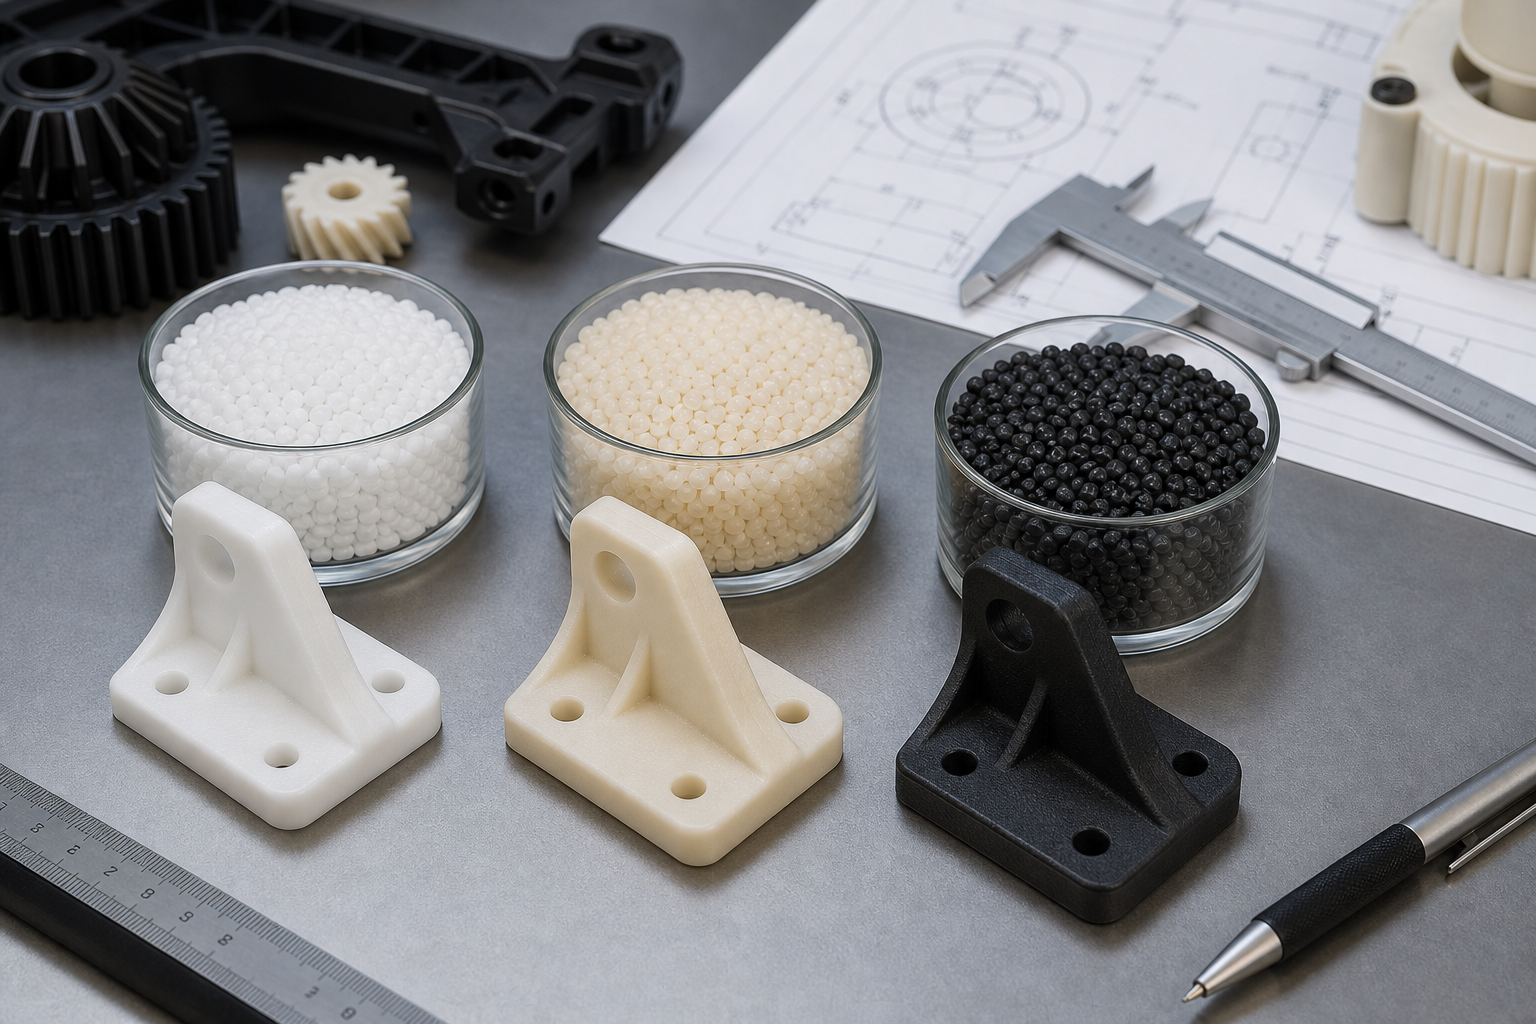
| Stiff brackets or housings | PA6 GF30 or PA66 GF30 | Higher stiffness and lower shrinkage, but more fiber-orientation risk |
| Wear parts | PA6, PA66 or lubricated nylon | Useful for gears, bushings and sliding components |
| Moisture-sensitive dimensions | PA12 or reinforced nylon | Better dimensional planning for humid environments |
When Nylon Injection Molding Is a Good Fit
Nylon is a strong choice for parts that need toughness, fatigue resistance, wear resistance and lower friction than commodity plastics can provide. Typical molded nylon components include gears, bushings, brackets, clips, housings, connectors, pump parts, automotive parts and industrial machine components.
Choose nylon injection molding when the part needs repeatable production, a stable geometry and a material that can handle mechanical stress. If the volume is low or the design is still changing, CNC machining or 3D printing may be better for early validation before tooling.
PA6 for Tough and Cost-Effective Parts
PA6 is often used when impact resistance, processability and cost balance are important. It is a practical choice for many general mechanical parts, but its moisture absorption must be considered for tight fits.
PA66 for Heat and Stiffness
PA66 is often selected for higher temperature applications and stronger stiffness. It can be a better option for under-hood automotive components, electrical housings and load-bearing parts.
Glass-Filled Nylon for Structural Components
Glass-filled nylon improves stiffness and dimensional stability, but it also increases tool wear and directional shrinkage. Gate location and fiber orientation become more important as glass content increases.
Tooling Requirements for Nylon Parts
Nylon molds need careful gate design, venting, cooling and ejection planning. Poor gate placement can create weak weld lines, fiber-rich surfaces, visible flow marks or warpage. For glass-filled nylon, mold steel and gate wear must also be considered.
| Tooling factor | What to check | Risk if ignored |
|---|---|---|
| ゲートの位置 | Flow direction, weld line location, appearance | Weak weld lines or warpage |
| 愚痴 | End-of-fill air traps and burn marks | Short shots or burned surfaces |
| 冷却 | Uniform mold temperature | Differential shrinkage |
| ドラフト角 | Ejection force and surface texture | Scratches, drag marks or sticking |
| Steel choice | Glass-filled nylon abrasion | Premature gate/cavity wear |
Tolerances and Moisture Absorption
Nylon absorbs moisture, and moisture changes dimensions and mechanical behavior. This does not make nylon unreliable, but it means tolerances must be defined with the final use condition in mind.
For tight dimensions, define whether inspection happens dry-as-molded, after conditioning or after a humidity exposure target. If an assembly must fit after shipping or field use, the tolerance plan should reflect that real state instead of only first-article inspection.
Common Nylon Molding Problems and Solutions
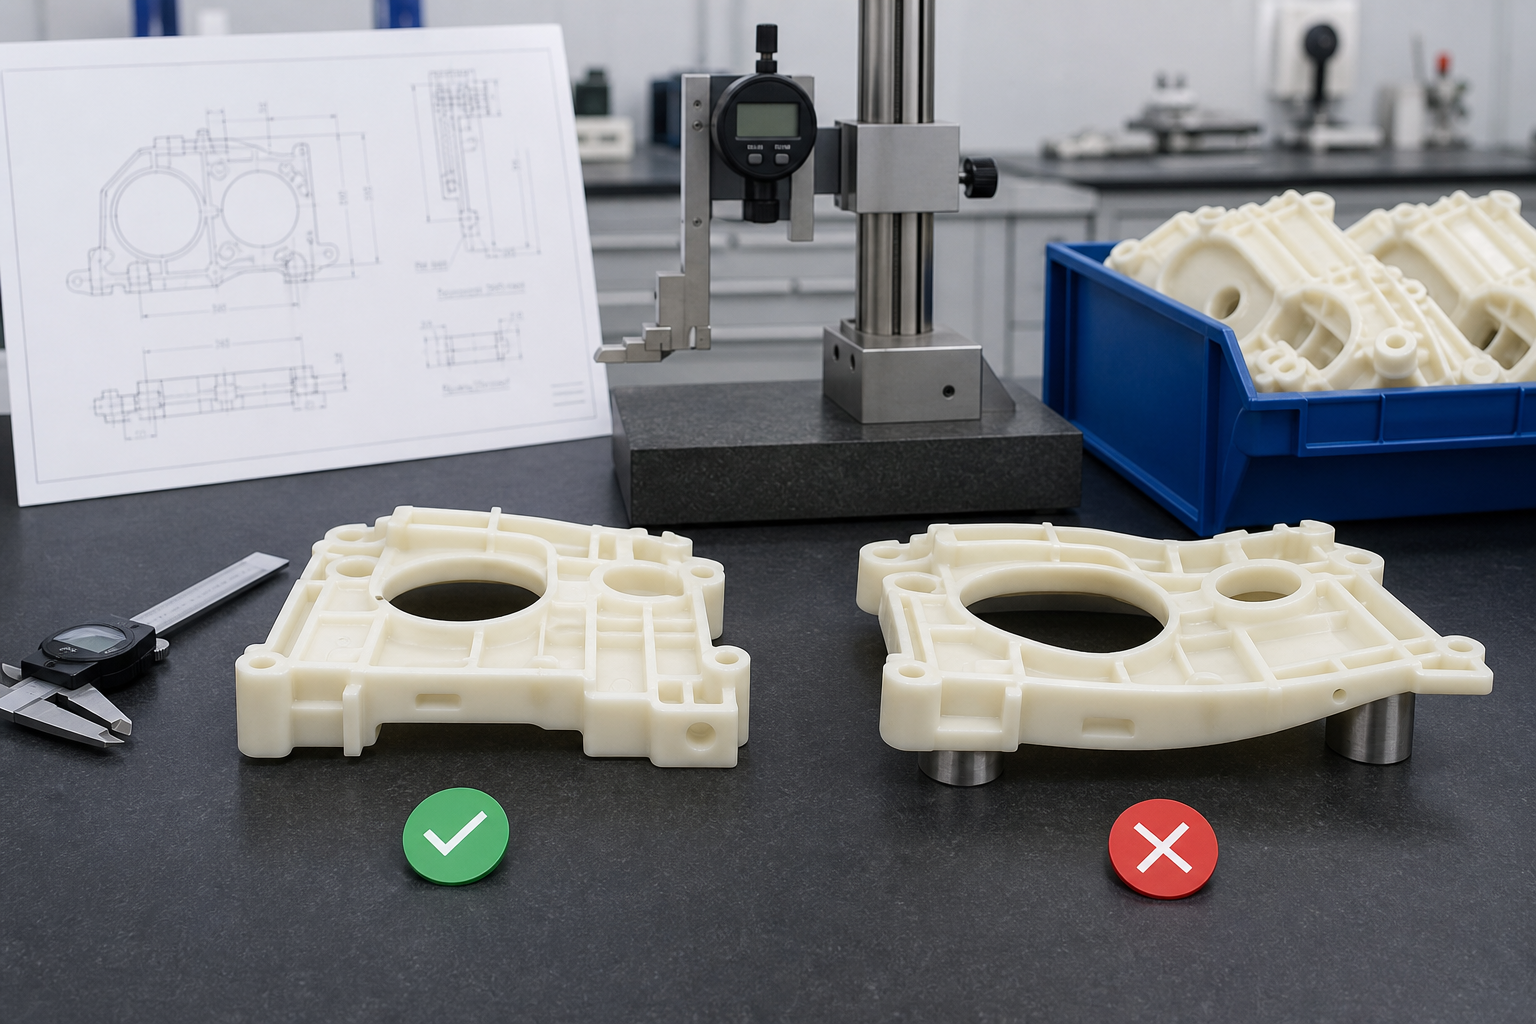
| 問題 | Common cause | Practical solution |
|---|---|---|
| Splay or silver streaks | Wet resin, overheating or contamination | Dry resin properly and control material handling |
| 反り | Uneven shrinkage, fiber orientation or poor cooling | Adjust gate location, wall balance and cooling |
| ショートショット | Low pressure, poor venting or thin flow paths | Improve vents, melt flow and wall thickness |
| Sink marks | Thick sections and poor packing | Core out thick areas and tune packing |
| 溶接線の欠陥 | Gate layout or low melt-front temperature | Move gates or improve melt and mold temperature |
関連記事
よくある質問
What is the best nylon for injection molding?
PA6 is often a good general-purpose nylon for tough molded parts, while PA66 is better when heat resistance and stiffness are more important. Glass-filled PA6 or PA66 can improve strength and dimensional stability, but the mold and part design must account for fiber orientation.
Is nylon injection molding suitable for tight tolerance parts?
Yes, but the tolerance plan must consider moisture absorption and measurement conditions. For critical dimensions, define whether the part is inspected dry-as-molded, conditioned or after a defined humidity exposure.
Does glass-filled nylon require special tooling?
Glass-filled nylon is more abrasive than unfilled nylon, so mold steel, gate design and wear areas should be reviewed carefully. Higher glass content usually increases tool wear and directional shrinkage risk.
What information should I send for a nylon molding quote?
Send CAD files, drawings, material requirements, annual volume, tolerance needs, surface finish, color, testing requirements and the real operating environment. If you are unsure about the material, describe the load, temperature, moisture and chemical exposure.
Can nylon parts be prototyped before injection molding?
Yes. CNC machining, SLS nylon 3D printing or prototype tooling can be used before production tooling. The best prototype method depends on geometry, quantity, tolerance and material requirements.
Can a nylon injection molding supplier support DFM review and material selection before tooling?
Yes. A capable supplier should review wall thickness, ribs, gates, draft, warpage risk and the operating environment before tooling starts. Early DFM and material guidance usually reduce mold changes, sampling delays and avoidable quality issues.
Can you provide inspection records, certificates or sample validation for nylon molded parts?
Yes, if those requirements are defined in the RFQ. Buyers commonly request material certifications, dimensional reports, first article inspection data, color references or sample approval before mass production, so the supplier should confirm that scope in advance.
詳細を比較する PA66 GF30の特性とグレード選定 当社のガラス繊維強化ナイロン専用ガイドにおいて、GF15、GF30、GF60の各ガラス繊維強化レベルについて。.
Request a Nylon Injection Molding Review
For a PA6, PA66 or reinforced-nylon production part, send the assembly and drawing revision, exact resin grade or permitted alternative, quantity by phase and service environment. Nylon Plastic can review grade, DFM, tooling, sampling and inspection before quotation.
依頼内容に含めるべき事項
- 3D CAD files and 2D drawings.
- Target material or performance requirements.
- Annual volume and first order quantity.
- Critical dimensions and tolerance requirements.
- Surface finish, color and texture expectations.
- Assembly, insert molding or post-processing needs.
- Testing requirements such as heat aging, load testing or chemical exposure.
- Packaging and logistics requirements.
- State reinforcement, color and applicable flame/electrical or regulatory requirements against the exact grade.
- Define critical dimensions and whether sample and production inspection use dry-as-molded or agreed conditioned parts.
- Specify first-article records, functional approval, cavity identification, material traceability, destination and packaging.
Nylon Plastic focuses on functional nylon parts where the material choice, tooling plan and production process all affect service life. For nylon injection molding, we review the resin family, part geometry and operating environment before tooling starts, so the quote is based on real manufacturing risk instead of a generic PA6 or PA66 assumption.
- Material selection support: compare PA6, PA66, PA12, glass-filled nylon, flame-retardant grades and modified compounds against load, heat, moisture and chemical exposure.
- DFM before tooling: review wall thickness, ribs, bosses, snap fits, gates, draft, weld lines and warpage risk before the mold is cut.
- Tooling and sampling control: align mold steel, gate strategy, drying conditions, process window and T1 sample feedback with the target part function.
- Production documentation: support RFQs that require material certificates, dimensional inspection, sample approval, color matching or batch-level quality checks.
If the design is not ready for production tooling yet, we can also compare ナイロンのCNC加工 または ナイロン3Dプリント as prototype or low-volume routes before moving into injection molding.
Ask the quote to separate tooling, cavity count, samples, molded parts, inserts or assembly, any conditioning, inspection and packaging. Confirm tool ownership and which qualification tests are included or arranged separately. Use production-intent resin and mating parts for the agreed approval; a generic nylon datasheet does not approve a finished assembly.