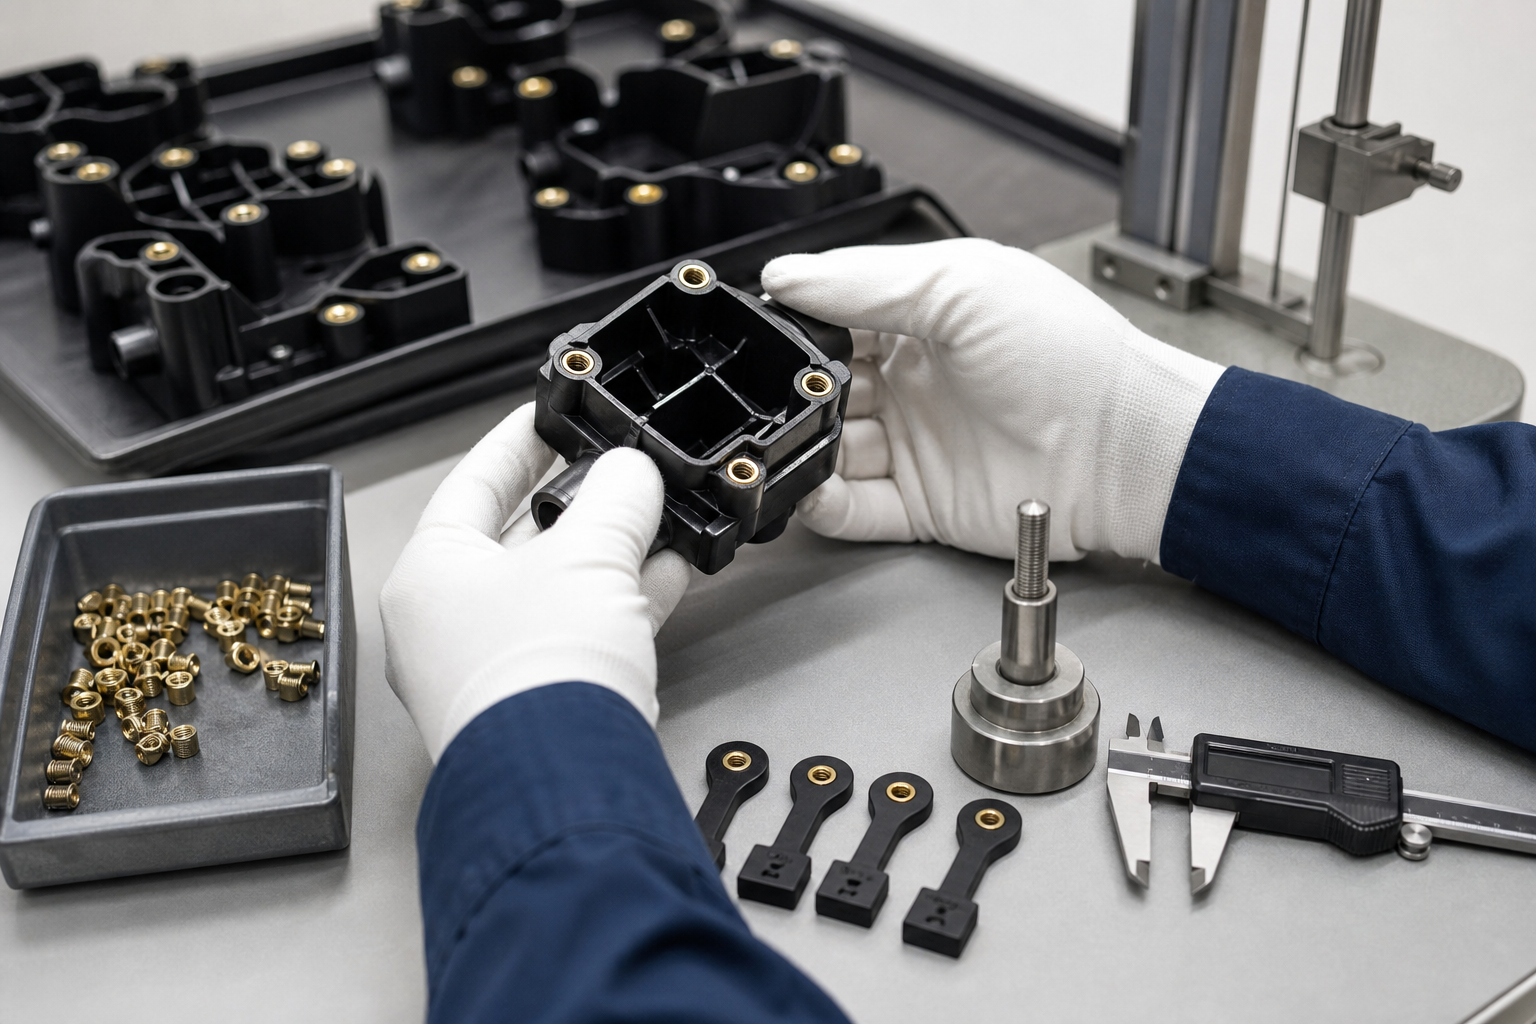
Metal insert molding is used when a plastic part needs metal threads, wear surfaces, reinforcement or electrical/structural integration without adding secondary assembly steps. Common examples include threaded bosses, electrical carriers, sensor housings, mounting points and load-bearing interfaces.
When the molded part also needs heat, chemical, or moisture stability, review ナイロンの化学的相容性表, ナイロンの吸湿性, そして ナイロンの耐薬品性 before insert retention and resin selection are finalized.
This guide explains how to source metal insert molded plastic parts, what design rules matter before tooling, and which supplier questions reduce the risk of loose inserts, cracked bosses and unstable production yield.
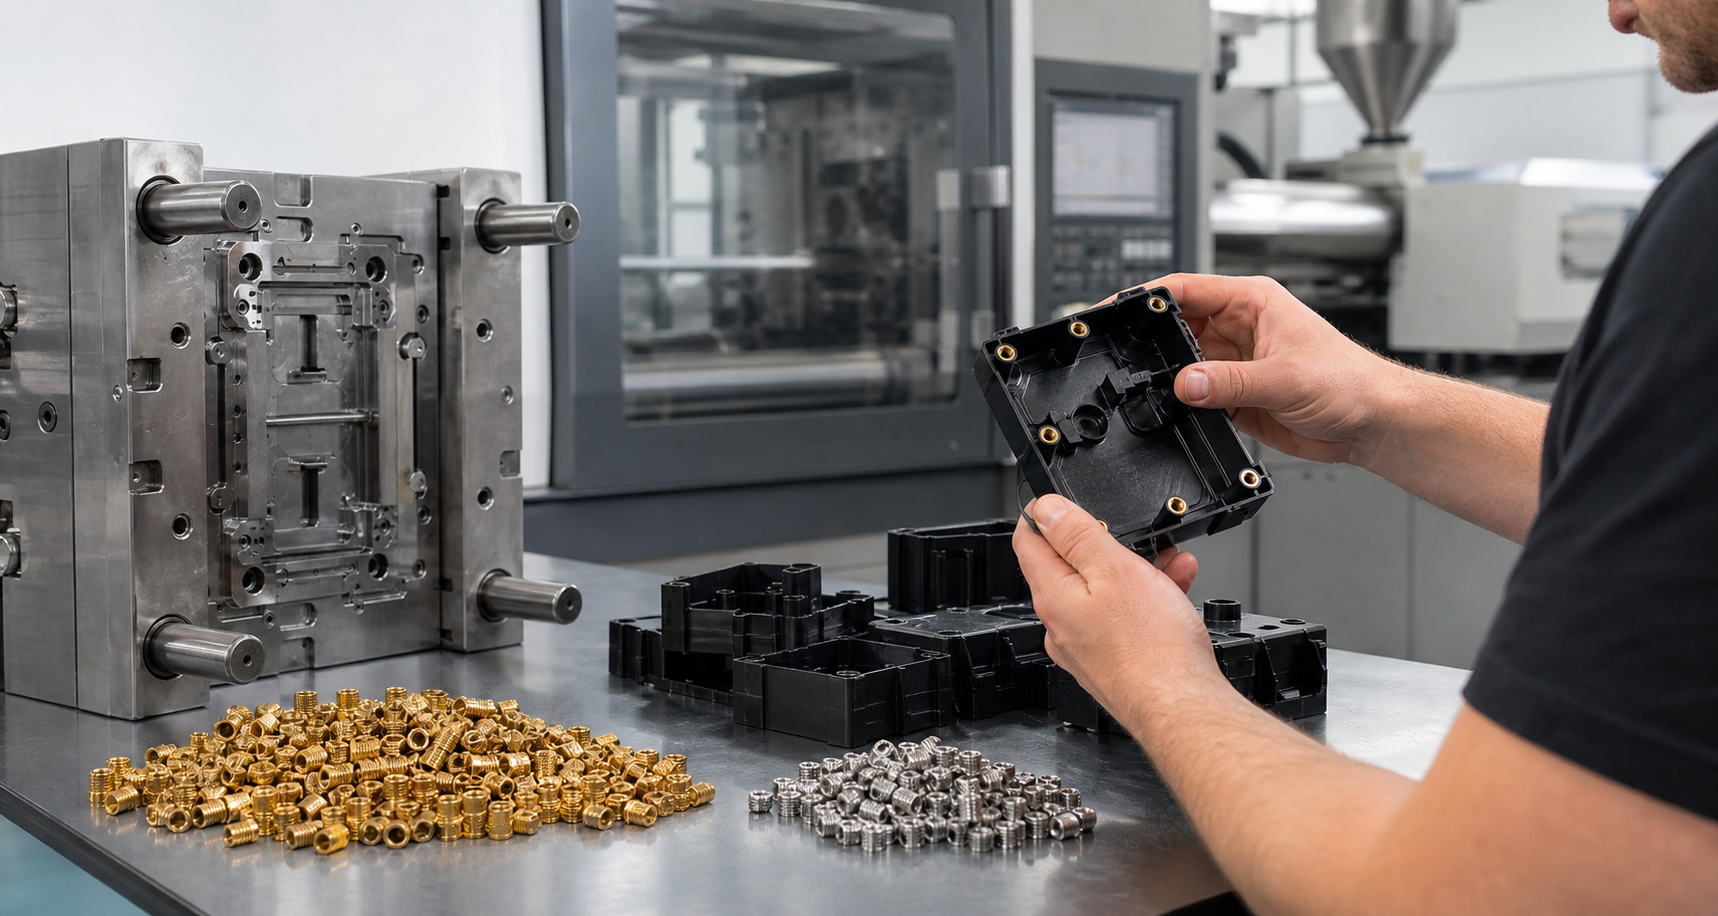
Metal Insert Molding at a Glance
| 意思決定領域 | Common Choices | 購入者確認 |
|---|---|---|
| Insert type | Brass threaded inserts, stainless bushings, pins, stamped contacts | Confirm pull-out, torque and corrosion requirements |
| Plastic materials | PA, PBT, PC, ABS, PPS, PEEK and filled engineering plastics | Match resin shrinkage and temperature to insert geometry |
| Tooling method | Manual loading, robotic placement, fixture-assisted positioning | Review cycle time and insert location stability |
| 主なリスク | Insert shift, resin flash, boss cracking, weak retention | Ask how the supplier validates retention and alignment |
| 見積依頼(RFQ)の入力内容 | Insert drawing, plastic part CAD, torque or pull-out need, quantity | Share both the plastic and metal requirements |
When Insert Molding Makes Sense
Insert molding is usually preferred when the program needs strong fastening points, reduced assembly time or better positional accuracy than a secondary heat-staking or press-in step can deliver. It is especially useful when the plastic part will be opened and reassembled repeatedly, or when threaded engagement must remain stable in production.
If the part only needs light-duty threads in a noncritical area, a simpler post-molding insert process may be enough. The correct decision depends on load, quantity, assembly method and tolerance stack-up.
Insert Types, Materials and Tooling Review
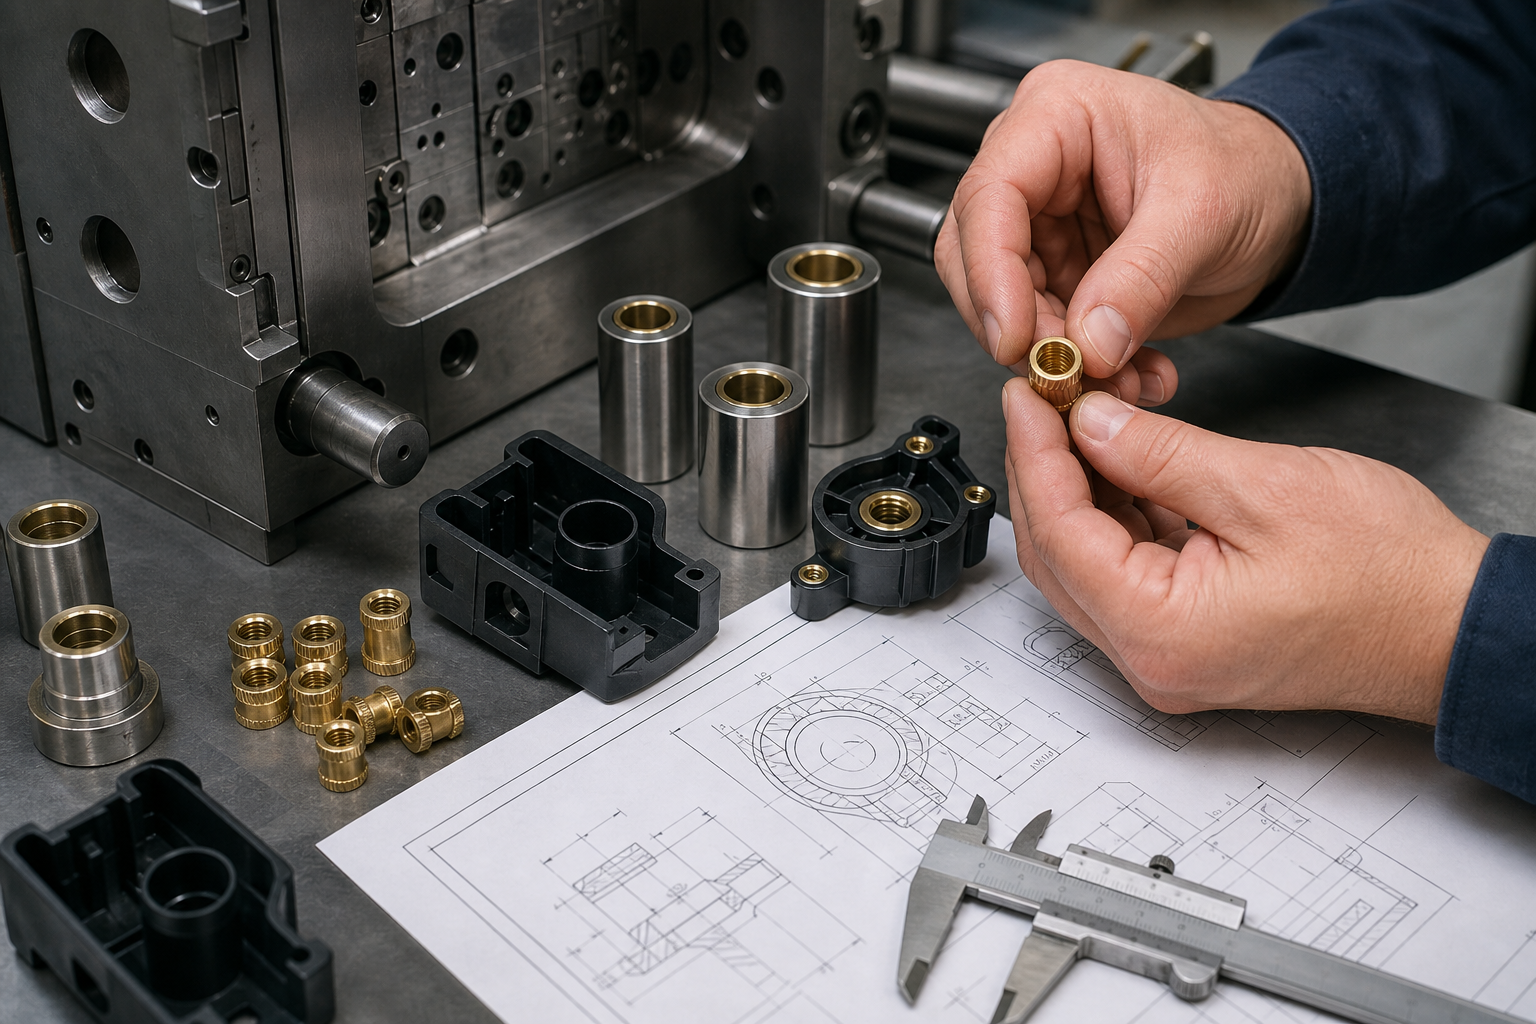
Brass inserts are common because they machine well and offer good thread performance. Stainless inserts may be chosen for corrosion or strength requirements. The surrounding plastic must be reviewed together with the insert shape, knurl geometry and molding temperature window.
- Confirm whether the insert will see torque, pull-out, vibration or thermal cycling.
- Review wall thickness around the insert before cutting steel.
- Check whether preheating or special loading fixtures are needed.
- Ask how insert position is controlled during molding.
Design Rules Before Tooling
- Avoid undersized bosses that leave no room for resin support around the insert.
- Keep inserts away from sharp stress risers and thin wall transitions.
- Share mating screw size, target torque and clamp load with the supplier.
- Review gate location so resin fills around the insert without voids or weld-line weakness.
- Confirm draft, ejection and cooling around heavy metal masses in the mold.
Common Problems and How to Reduce Them
| 問題 | 考えられる原因 | Reduction Method |
|---|---|---|
| シフトを挿入 | Poor loading control or unstable fixture support | Use reliable placement tooling and validate position early |
| Boss cracking | Insufficient resin support or wrong torque expectation | Increase support geometry and confirm assembly load |
| Weak retention | Wrong insert geometry or process window | Define pull-out requirement and test the actual molded part |
| Long cycle time | Manual insert loading with high labor content | Review automation or part-family strategy before launch |
関連記事
よくある質問
What is metal insert molding used for?
It integrates metal threads, bushings, pins or contacts directly into a molded plastic part so the assembly can handle fastening, wear or structural load with fewer secondary operations.
Are brass inserts better than stainless inserts?
Brass is common for threaded retention and processing ease. Stainless may be better when corrosion resistance, temperature exposure or a specific mechanical requirement is more important.
What should I send for an insert molding quote?
Send the plastic CAD model, insert drawing or sample, annual quantity, screw specification, assembly load and any pull-out, torque or dimensional requirement.
How do suppliers test insert retention?
Typical checks include pull-out testing, torque testing, dimensional inspection and first-article validation against the part drawing and assembly method.
Can insert molding use reinforced nylon?
Yes, PA-GF20 and PA-CF30 can be considered when stiffness, wear or thermal performance is needed. The supplier should review fiber orientation, insert temperature, boss support, shrinkage and retention data before tooling release.
Request a Metal Insert Molding Review
Send the plastic-part and metal-insert drawings together, with the resin grade, assembly load and quantity. Nylon Plastic can review insert positioning, tooling, retention, inspection and alternative manufacturing routes before quotation.
依頼内容に含めるべき事項
| Ask For | なぜ重要なのか |
|---|---|
| Insert and plastic drawings together | Tooling cannot be reviewed correctly from one side only |
| Retention requirement | Defines whether pull-out or torque testing is needed |
| Assembly method | Confirms screw engagement and service condition |
| Annual volume | Guides fixture, automation and cycle-time decisions |
| First article and validation plan | Reduces launch risk before mass production |
- Identify insert material, plating, tolerances, presentation and who supplies each insert; include thread or contact areas that must remain free of flash.
- Define pull-out, torque, position, seal or electrical requirements, sampling and any environmental test.
- Include assembly/mating data, first-article report, traceability, destination and packaging.
Nylon Plastic supports engineering plastic part development with DFM review, insert molding planning, tooling discussion and broader manufacturing comparison when a part may also be viable through machining or secondary assembly. That helps buyers avoid locking into the wrong integration method too early.
Compare the same insert supply, fixture/loading or automation, mold and sampling, molded-part inspection and packaging scope. Confirm who provides inserts and test fixtures and who handles rejected inserts or molded assemblies. Approve retention and functional sample criteria before repeat production; nominal insert dimensions alone do not establish a robust joint.