For engineering and production teams
Nylon Injection Molding Process Review
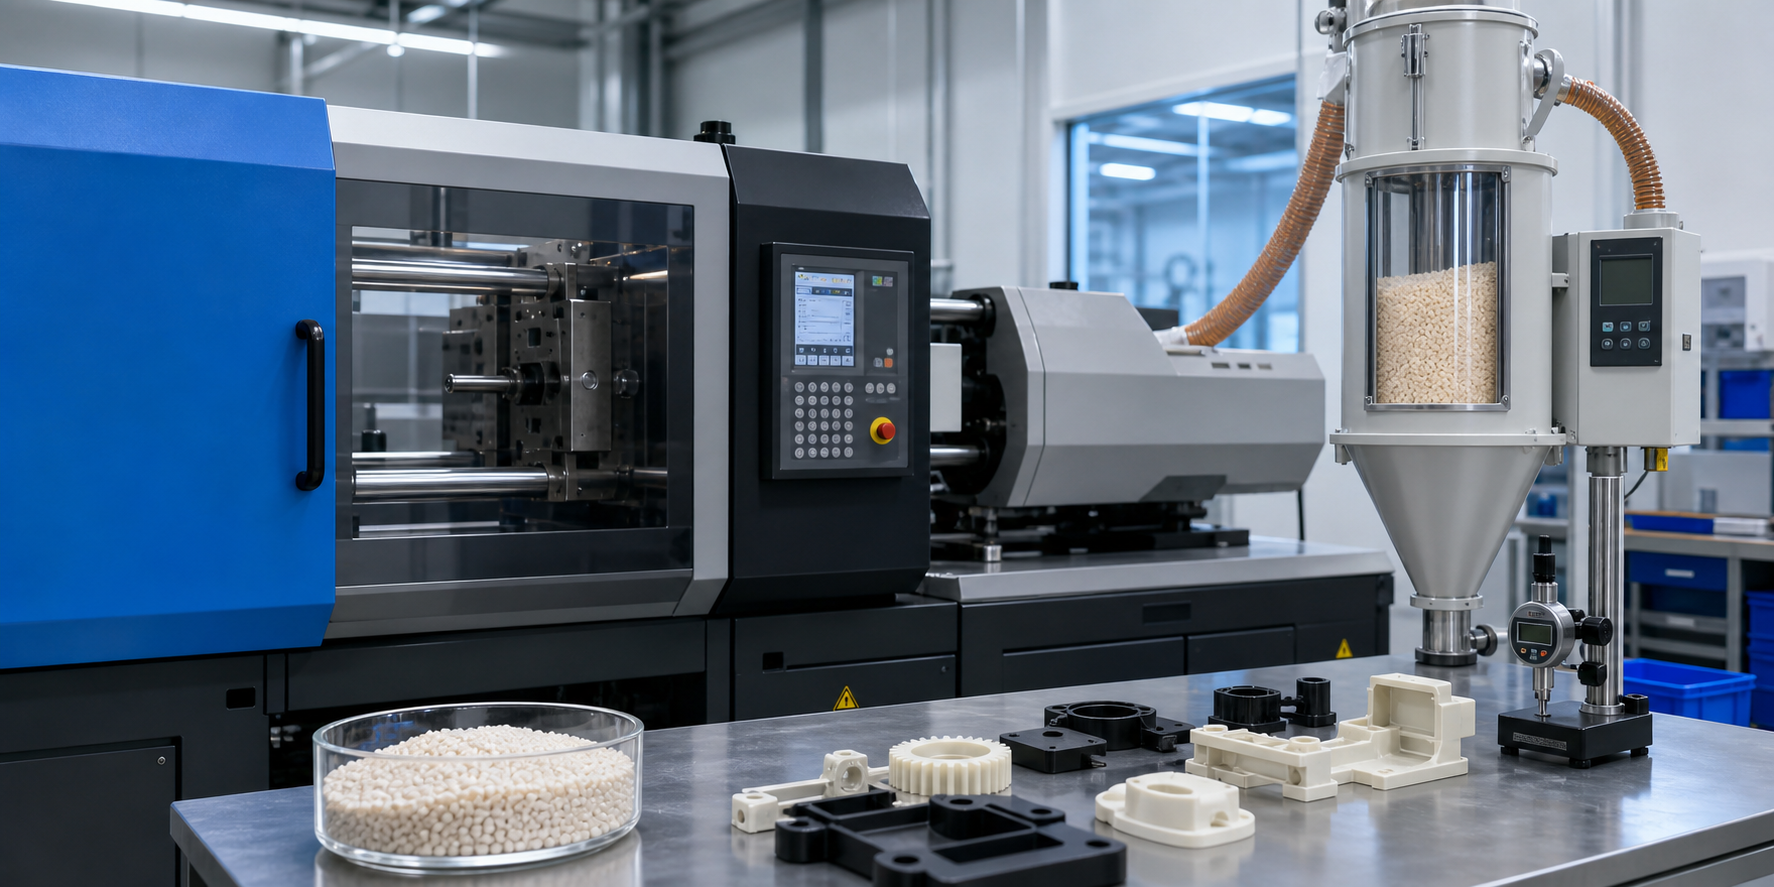
ナイロン射出成形 requires coordinated control of resin moisture, melt and mold temperature, fill and pack conditions, cooling and the measurement state. The working window must be validated for the exact PA6, PA66, PA12 or reinforced grade and the actual part geometry.
- Record incoming moisture and drying conditions by batch
- Set melt, mold, fill and pack conditions as one validated window
- Inspect warpage and dimensions in the agreed conditioning state
Nylon Injection Molding at a Glance
| 決断の分かれ目 | Processing Takeaway | Approval Check |
|---|---|---|
| 乾燥 | Critical for quality | Moisture control is a must before molding |
| Tooling heat | Stability matters | Use consistent mold and barrel conditions |
| 反り | Common risk | Gate, wall and cooling choices matter |
| 最適な用途 | Functional molded nylon parts | Lock process window before volume production |
Why Nylon Injection Molding Needs Grade-Specific Control
Nylon grades are moisture-sensitive and semicrystalline, so material preparation, flow, shrinkage and conditioning can change both appearance and measured dimensions. Reinforcement, color package and part geometry can shift the usable process window again.
The main controls are:
- Moisture condition: use the resin supplier’s limit for the exact grade, record drying and protect the material during transfer.
- Fill and temperature window: confirm melt, mold, speed and pressure together; changing one value can move weld lines, flash, burn marks or packing behavior.
- Shrinkage and warpage: review gate direction, fiber orientation, wall transitions, cooling and the agreed conditioning state before approving dimensions.
A stable trial links the material lot and preparation record to the machine settings, mold configuration and measured part results. A generic temperature table alone does not approve a production process.
主要な処理パラメータ
The ranges below are preliminary screening values for process planning. Confirm the current supplier data for the exact resin grade, reinforcement, color and machine, then validate the window on the molded part. Do not use a generic range as the final production specification.
| パラメータ | PA6 | PA66 | PA12 | PA6-GF30 | PA66-GF30 |
|---|---|---|---|---|---|
| 溶融温度(°C) | 230-260 | 270-290 | 240-270 | 240-270 | 280-300 |
| 金型温度(°C) | 60-80 | 80-100 | 40-60 | 80-100 | 80-110 |
| ノズル温度(°C) | 230-260 | 270-290 | 240-270 | 245-275 | 285-300 |
| Front Zone (°C) | 230-250 | 265-280 | 235-255 | 235-255 | 270-285 |
| Middle Zone (°C) | 235-255 | 270-285 | 240-260 | 240-260 | 275-290 |
| Rear Zone (°C) | 230-250 | 265-280 | 235-255 | 235-255 | 270-285 |
| Drying Temp (°C) | 80-85 | 80-85 | 80-85 | 80-85 | 80-85 |
| Drying Time (hrs) | 4-6 | 4-6 | 4-6 | 4-6 | 4-6 |
射出および圧力パラメータ
Beyond temperature, injection pressure and speed are critical for filling nylon molds properly. Nylon’s high viscosity requires higher pressures than polypropylene, but excessive pressure causes flash and mold wear.
| パラメータ | PA6 | PA66 | PA6-GF30 | 備考 |
|---|---|---|---|---|
| 射出速度 | 中~高 | 中~高 | ミディアム | Fast fill to minimize air entrapment |
| Injection Pressure (MPa) | 80-120 | 100-140 | 100-150 | Higher for thin walls |
| Holding Pressure (MPa) | 40-60 | 50-80 | 50-70 | 60-80% of injection pressure |
| Back Pressure (MPa) | 0.3-0.5 | 0.3-0.5 | 0.5-0.8 | Low for nylon to avoid shear degradation |
| Cooling Time (s/mm) | 0.8-1.0 | 0.8-1.0 | 1.0-1.2 | Thicker parts need more time |
| Screw Speed (rpm) | 50-80 | 50-80 | 30-50 | Lower for reinforced grades |
よくある不具合と解決策
Understanding the root causes of nylon defects allows targeted solutions rather than guesswork:
- Splay (silver streaks): Caused by moisture or volatile contaminants. Solution: Dry material thoroughly, purge with nylon-specific purge compound, check vent zones.
- Weld lines: Occur where two flow fronts meet. Solution: Increase melt temperature, raise injection speed, add gas vents at weld line locations.
- ショートショット: Caused by insufficient flow length or low pressure. Solution: Increase injection speed and pressure, raise melt temperature, redesign gate location.
- 反り: Results from uneven shrinkage. Solution: Increase mold temperature, balance wall thickness, add ribs for stiffness, use symmetric gating.
- Bubble formation: Indicates moisture, air entrapment, or material degradation. Solution: Verify drying, lower back pressure, check for insufficient venting.
サイクルタイムの最適化
Nylon cycle time is dominated by cooling requirements. Since nylon molds at elevated temperatures (60-110°C vs 20-40°C for PP), significantly more cooling time is needed. Optimizing cooling is the most effective way to reduce cycle time for nylon parts.
- Mold cooling design: Baffle and bubbler cooling channels positioned 1.5x the cavity depth from the parting surface
- Cooling water temperature: Use chilled water (8-15°C) for large or thick nylon parts to reduce cycle time by 15-30%
- Ejection temperature: Parts should reach 60-80°C at ejection to minimize warpage
- Hot runner optimization: Nylon requires precise hot runner temperature control (within ±2°C) to prevent material degradation in the runner
材料の切り替えとパージ
When switching from nylon to another material (or vice versa), proper purging prevents contamination and equipment damage. Nylon leaves significant residue in the barrel due to its adhesive nature.
- Purging from nylon: Use PA-specific purge compound or polypropylene as a purging agent at processing temperatures 20°C above nylon melt temperature
- Purging to nylon: Ensure barrel is completely clean of previous material; purge with nylon-compatible intermediate material
- 色の変化: Perform two full barrel purges with natural material before adding color concentrate
For a project-specific review, share the resin grade, part drawing, defect photos and the current drying and process record. Nylon Plastic can compare material, DFM and trial requirements before quotation.
Moisture and Shrinkage Checks Before Process Approval
A stable machine setting is not enough to approve a molded nylon part. The trial record should connect incoming moisture, flow direction, shrinkage and conditioning state to the drawing dimensions. Otherwise, a parameter change may hide the real source of splay, warp or dimensional drift.
| Check | PA6 | PA66 | Reinforced nylon | Approval evidence |
|---|---|---|---|---|
| Pre-molding moisture target | Confirm against the resin supplier; the merged process reference used 0.20% maximum | Confirm against the resin supplier; the merged process reference used 0.15% maximum | Confirm the exact GF/CF grade; the merged reference used 0.12% maximum | Moisture reading, dryer set point, drying time and sealed-transfer record |
| Directional shrinkage | Review flow and cross-flow dimensions separately | Review flow and cross-flow dimensions separately | Expect fiber orientation to increase directional behavior | Cavity-specific measurements with flow direction marked on the report |
| Conditioning state | Record dry-as-molded versus conditioned measurement | Record dry-as-molded versus conditioned measurement | Use the same conditioning definition for every trial | Measurement time, temperature, humidity and acceptance condition |
| Corrective action | Separate material preparation, fill/pack, cooling and tooling changes instead of adjusting several variables at once | Controlled trial sheet showing one change and one observed result per step | ||
These values are starting references, not universal specifications. Resin supplier data, reinforcement level, color package, recycled content, wall thickness and mold design can change the allowable moisture and shrinkage window. Project teams should require the molder to state the tested grade and conditioning method in the sample-approval record.
このプロジェクトにおいて、ナイロンプラスチックでどのようなカスタマイズが可能か
ナイロンプラスチック社は、材料の改質に加え、製品設計、金型設計・製作、射出成形、CNC加工、3Dプリントを統合しています。適切な適用範囲は、一般的な材料名から安易に決定するのではなく、図面や使用条件に基づいて選定されます。.
| カスタマイズエリア | 検討すべき選択肢 | 必要な情報 |
|---|---|---|
| Material preparation | Grade review, drying and sealed material-handling plan | Resin grade, supplier data and incoming moisture condition |
| Tool and DFM | Gate, vent, cooling, draft, ejection and shrinkage review | CAD, drawing, cosmetic zones and critical dimensions |
| Process development | Melt, mold, fill, pack and cycle-window validation | Defect history, machine constraints and sampling quantity |
| Production support | Molding, inspection, documentation and packaging planning | Annual volume, acceptance criteria and delivery requirements |
見積依頼(RFQ)チェックリスト
- Exact nylon grade, reinforcement and color
- CAD and drawing with critical and cosmetic requirements
- Service temperature, humidity, load and chemical exposure
- Existing defects, sample parts or current process data if available
- Sampling quantity, annual volume and required inspection documents
DFMのサポート、NDAの取り決め、材料や組成に関する文書、および検査要件については、見積りの際に協議可能です。提供の可否は、プロジェクトの範囲および合意された品質計画によって異なります。.
レビューから本番環境へ
- 定義: 図面、アプリケーション、環境、およびボリュームを共有する。.
- レビュー: 材料、プロセス、DFM、および検証に関するリスクを比較する。.
- 検証: 必要に応じて、サンプル、3Dプリント、CNC加工、または試作金型を活用する。.
- 制作: 合意された検査が完了してから、金型や生産を開始すること。.
よくある質問
Which nylon grades can be reviewed for injection molding?
Nylon Plastic works across engineering plastic material selection and injection molding. The review can compare PA6, PA66, PA12 and reinforced options when the exact grade has not been locked.
Can the drying and molding window be developed for a specific part?
Yes, but it must be based on the exact resin, wall thickness, gate, machine and quality targets. Generic temperatures are a starting point, not a validated production window.
What is included in a nylon molding DFM review?
The review can cover material behavior, wall transitions, ribs and bosses, draft, gate and weld-line risk, cooling, ejection, shrinkage, warpage and the inspection condition.
Can Nylon Plastic support prototypes before volume molding?
The site presents product design, 3D printing, CNC, mold making and injection molding capabilities. The appropriate sequence depends on whether the team needs geometry proof, functional samples or production-equivalent molded parts.
関連記事
技術情報源および検証
サプライヤーのデータを用いて、正確なグレードおよび試験条件を確認してください。最終承認は、製造プロセス、部品の形状、および使用環境を反映したものである必要があります。.
- BASF Ultramid nylon technical and processing downloads
- Verified PA6 and PA66 grade datasheet library
- PA6 properties and grade-selection guide
- PA66 properties and grade-selection guide
Request a Nylon Injection Molding Review
Send the part drawing or CAD, exact resin grade where known, critical dimensions, service conditions, current defects, sample quantity, annual volume and required inspection records. The review can cover material choice, DFM, tooling and the trial plan before quotation.
A useful nylon injection molding review connects the grade, dryer control, gate and cooling design, dimensional condition and production requirement. Review the nylon injection molding service or upload the project files below.