Rapid tooling vs production tooling is a project-stage decision. Choose rapid tooling for fast molded parts, expected design changes, or launch bridging. Choose production tooling when the design, resin, demand, tolerances, and quality plan are stable enough to justify a longer-life manufacturing asset.
Buyers should compare mold build time, expected shots, cavity output, cycle time, maintenance, change risk, part price, and the cost of delaying validation or launch.

Where Rapid Tooling Fits
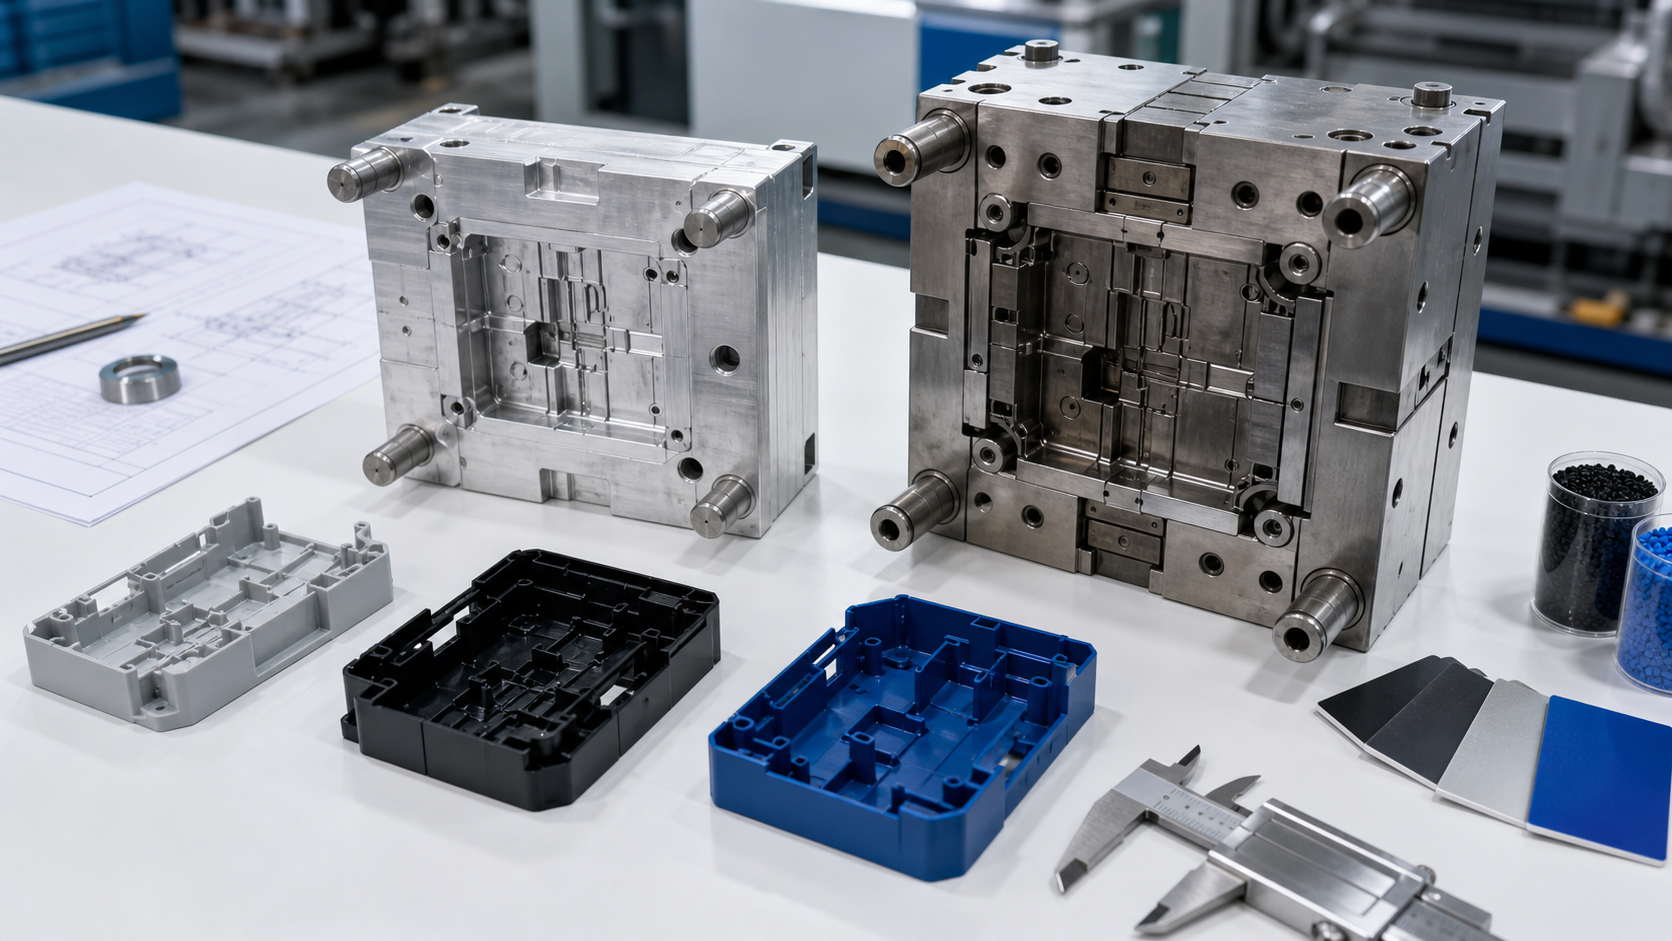
Rapid tooling is commonly used for engineering validation, pilot builds, market trials, low-volume orders, and bridge production. The mold may use aluminum, pre-hardened steel inserts, a standard mold base, manual inserts, or simplified automation. Its purpose is to obtain representative injection-molded parts without committing immediately to every feature of a long-life production mold.
This route is valuable when the project must validate shrinkage, warpage, sink, weld lines, gate appearance, snap fits, sealing surfaces, or assembly behavior in the intended resin. A machined or printed prototype can answer many geometry questions, but it does not fully reproduce molding orientation, residual stress, or process-dependent dimensions. For earlier process selection, use our plastic prototype manufacturing guide.
「」を使用してください。 low-volume injection molding guide when the pilot or bridge requirement is a limited batch of molded parts.
Where Production Tooling Fits
Production tooling is designed around repeatable output over the expected program life. It normally includes steel selected for the resin and shot requirement, production cooling, durable shutoffs and wear surfaces, stable ejection, defined venting, and provisions for maintenance or automation. Multi-cavity layouts and hot runners may be justified when their cycle-time and material savings support the volume.
Choose this route when released drawings are controlled, annual demand is credible, critical dimensions have an inspection method, and the product team can approve a final gate, parting line, texture, and ejection strategy. Abrasive glass-filled resins, corrosive materials, high-temperature processing, or demanding cosmetic surfaces also increase the value of a correctly specified production tool. The 工具鋼の選定ガイド explains the related steel tradeoffs.
について mold fabrication guide sets out the design, sampling and inspection scope to agree before tool release.
Cost, Mold Life, and Lead Time Comparison
| 決定要因 | 迅速なツーリング | Production tooling |
|---|---|---|
| Primary objective | Fast learning, launch support, or limited production | Stable recurring production and lower long-run part cost |
| Typical build window | Often about 2-6 weeks | Often about 6-16+ weeks |
| Upfront cost | Lower; simplified construction and fewer production features | Higher; durability, cooling, automation, and capacity are engineered in |
| Indicative mold life | Thousands to tens of thousands of shots; design-dependent | Hundreds of thousands or more when correctly specified and maintained |
| Cavitation and output | Usually one or a few cavities | Selected from demand, press capacity, cycle time, and part-cost targets |
| Design revisions | Generally faster and less expensive before hardening | More disruptive after steel, texture, cooling, and automation are finalized |
| Piece-price trend | Often higher because of lower cavitation and more manual handling | Usually lower at sustained volume |
| Maintenance expectation | More frequent monitoring as shot count rises | Planned preventive maintenance with replaceable wear items |
These ranges are planning references, not guarantees. Part size, actions, texture, hot runners, resin, tolerance, cavity count, and validation requirements can change them. Ask suppliers to state assumptions beside cost and life estimates so quotes describe equivalent tools.
「」を使用してください。 射出成形のコストガイド to separate the tooling investment from recurring part costs when comparing quotations.
Choose the Route by Project Situation
| プロジェクトの状況 | Preferred route | 理由 |
|---|---|---|
| Geometry or assembly is still changing | 迅速なツーリング | Lower-cost modifications preserve learning speed |
| Pilot order is needed before a launch decision | 迅速なツーリング | Produces representative molded parts without full production commitment |
| Final tool is late but approved parts are required | Bridge rapid tool | Supports supply while the production tool is completed |
| Low annual demand may remain permanent | Rapid or low-volume steel tool | A high-cavity hardened mold may never recover its added cost |
| Demand, drawing, resin, and quality plan are stable | Production tooling | Longer life and faster cycles reduce program cost |
| Abrasive resin or tight uptime requirement | Production tooling | Wear-resistant components and maintenance planning protect continuity |
When to Move from Rapid to Production Tooling
Do not wait for a rapid tool to fail. Start the production-tool decision when forecast demand becomes repeatable and the economics of extra cavities, faster cooling, less manual labor, and lower maintenance outweigh the additional mold investment. Useful warning signs include rising flash, dimensional drift, frequent insert repair, slow cycle time, unstable cosmetic quality, or capacity that cannot meet the delivery plan.
Before freezing the production design, transfer the evidence learned from the rapid tool: actual shrinkage, warpage direction, gate performance, fill balance, venting needs, ejection marks, cooling behavior, assembly results, and inspection data. Confirm which dimensions require capability studies and which can be controlled through fixture design or normal inspection. Review the 許容差の累積に関するガイド before assigning unnecessarily tight tolerances to the mold.
よくある質問
What is the main difference between rapid and production tooling?
Rapid tooling prioritizes launch speed, change flexibility, and pilot volumes. Production tooling prioritizes long life, cavitation, automation, repeatability, maintenance, and lifecycle cost.
Can rapid tooling make production-quality parts?
Yes, when tool construction, resin, process, and inspection match the requirement, although tool life, cycle, cavitation, and automation may differ.
When should rapid tooling be skipped?
Go directly to production tooling when design and resin are proven, demand is reliable, validation is released, and a separate rapid tool would not reduce meaningful risk.
What must transfer into the production mold?
Transfer shrinkage, warpage, gate and vent results, cycle observations, cosmetic and assembly findings, dimensional reports, approved settings, maintenance lessons, and accepted design changes.
Request Comparable Tooling Options
For rapid tooling vs production tooling, share quantities by project phase and the decisions still open. Nylon Plastic can review the resin, DFM, sampling, wear, maintenance and production-transfer requirements on a common basis.
見積書の作成前に盛り込むべき事項と合意すべき事項
- 3D CAD, controlled 2D drawing, revision level, and intended resin grade.
- Prototype quantity, first production order, annual forecast, and program life.
- Critical dimensions, cosmetic zones, texture, color, and acceptance samples.
- Required launch date and whether bridge production must run in parallel.
- Requested cavity count, press constraints, cycle-time target, and automation needs.
- Tool ownership, mold steel and hardness, expected mold life, maintenance responsibility, and spare inserts.
- Qualification deliverables such as dimensional reports, material records, process parameters, and sample quantities.
A clear RFQ lets our engineering team separate optional features from required controls and explain whether rapid, bridge, or production tooling provides the lowest controlled project risk. For molded-part production requirements, see our injection molding capabilities.
Keep the comparison consistent. Specify the same mold base, steel and hardness, cavitation, runner, cooling, automation and validation scope. Include ownership, storage, transfer rights and spare inserts. Filled, flame-retardant, corrosive or optical materials may change wear, venting or polish requirements.
Ask for tooling investment and recurring part prices separately, with cavity output, validation work, expected life assumptions and transfer scope stated. Approve the samples and the conditions for moving into production before committing to the next tool.